Selecting the right concrete admixture can be the difference between a structure that merely meets specifications and one that exceeds durability and strength benchmarks. For projects requiring high fluidity and reduced water consumption, Polycarboxylate Ether (PCE) has emerged as the primary technical choice for modern engineering.
The shift toward high-performance concrete is driven by the need for increased compaction and lower permeability, which traditional water-reducers often struggle to achieve without compromising structural integrity. This requires a precise chemical balance that only a specialized pce factory can provide through controlled polymerization.
This article examines the technical mechanisms of PCE, the critical parameters for quality evaluation, and how to optimize dosage for various cementitious systems to ensure maximum structural longevity.


Historically, concrete fluidity was managed using lignosulfonates or naphthalene-based agents. While effective, these early generations required higher dosages and often led to excessive air entrainment or retardation of setting times. The transition to Polycarboxylate Ether (PCE) represented a paradigm shift from simple electrostatic repulsion to a combination of steric hindrance and electrostatic effects.
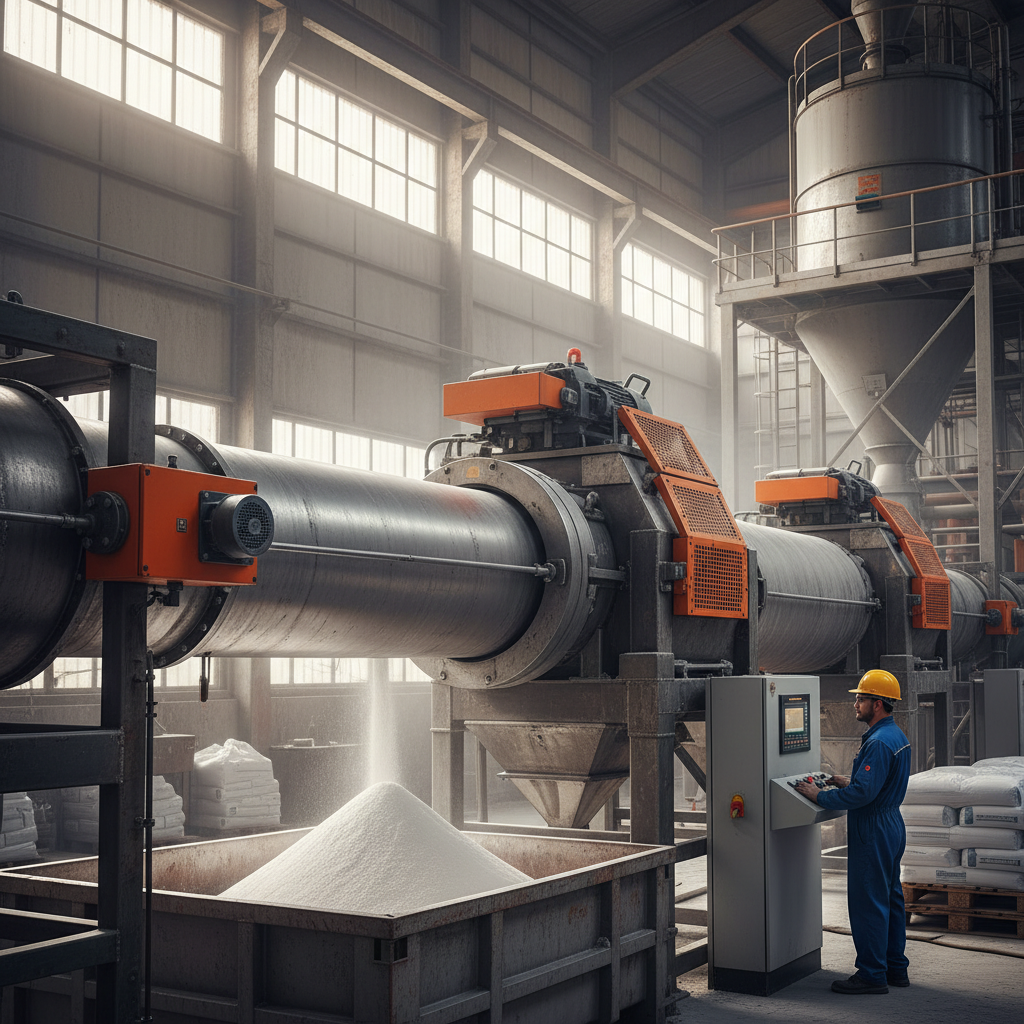
Modern production in a professional pce factory focuses on the precise architectural design of the polymer chain. By adjusting the length of the side chains and the distribution of the carboxyl groups, manufacturers can now tailor the admixture to specific cement types, ensuring that the fluidity is maintained without the risk of segregation.
PCE works by adsorbing onto the surface of cement particles. Unlike older superplasticizers that relied purely on negative charges to push particles apart, PCE molecules possess long polyethylene glycol (PEG) side chains. These chains create a physical barrier—steric hindrance—that prevents the cement particles from agglomerating, even at very low water-to-cement ratios.
This mechanism allows for a significant reduction in the amount of mixing water required to achieve a workable slurry. When water consumption is lowered, the resulting concrete matrix is denser, with fewer capillaries, which directly increases the compressive strength and reduces the permeability of the hardened mass.
The adaptability of this chemical structure is critical. Because different cement brands have varying proportions of C3A and C3S, the PCE must be formulated to maintain a stable adsorption layer. This ensures that the concrete remains fluid during transport and placement while setting predictably once the chemical reaction initiates.
Evaluating the quality of a PCE product requires looking beyond simple fluidity. Key technical indexes define the product's efficiency, including its effective content, chloride ion levels, and pH value. High-quality PCE is typically a white powder with an effective content of ≥95% and a water reduction rate of ≥25%, ensuring that small dosages yield significant results.
The effectiveness of PCE is not solely determined by the water reduction rate, but by the balance between slump retention and early strength development, minimizing shrinkage and creep performance in hardened slurry.
Furthermore, purity is paramount. Chloride ion content must be kept extremely low (typically ≤0.1%) to prevent the corrosion of steel reinforcement in reinforced concrete. A pH value between 6 and 8 ensures that the admixture does not adversely react with other components of the cementitious system, maintaining the chemical stability of the mix.
To understand the impact of PCE, one must analyze the relative performance across different concrete grades. High-performance concrete requires a higher water reduction rate to achieve the necessary density. In a typical industrial setting, the recommended dosage of PCE ranges from 0.10% to 0.40% of the cementitious material, depending on the target water reduction.
The following analysis illustrates a conceptual performance index where higher values indicate better efficiency in reducing water while maintaining fluidity. Note that these values are relative indicators used to compare the efficacy of different formulation strategies.
PCE is exceptionally versatile, making it suitable for Portland series cement concrete systems. It is widely utilized in ordinary concrete for residential builds, high-performance concrete for skyscrapers, and mass concrete for dams. In scenarios involving large amounts of fly ash or ore powder, PCE's high adaptability helps maintain fluidity despite the higher fine-particle content, which would otherwise increase water demand.
For optimal results, the mixing method is critical. While PCE can be added directly to the concrete, mixing it with water first—or adding it after the initial concrete mix—often yields a better effect. Users should ensure the homogeneity of the powder if pre-mixing in dry form to avoid localized concentrations that could lead to unpredictable setting times.
The industry is moving toward "Green Environmental Protection" formulations. Modern PCE production emphasizes the elimination of harmful substances and the reduction of volatile organic compounds (VOCs). By reducing the water-to-cement ratio, PCE indirectly contributes to sustainability by allowing for a higher replacement of cement with industrial by-products like slag and fly ash without losing strength.
Future developments are focusing on "smart" PCE molecules that can trigger release at specific time intervals, extending the slump retention for long-distance transport in hot climates. This reduces the need for additional retarders, simplifying the chemical cocktail and reducing the environmental footprint of the construction site.
Furthermore, the integration of one-stop sourcing services, as seen with Shijiazhuang Yaguan New Material Technology Co., Ltd., allows for customization of these products based on the specific mineralogy of the local aggregates and cement, ensuring that the most efficient (and thus most sustainable) dosage is used.
When evaluating a supplier or a specific product, a structured framework is necessary to avoid common pitfalls. Buyers should not look at the price per kilogram alone but rather the "cost per percentage of water reduction." A higher-quality PCE may have a higher unit price but requires a significantly lower dosage to achieve the same fluidity.
The trade-off between early strength and slump retention is another key consideration. Some PCE formulations provide rapid strength gain, ideal for precast concrete factories, while others are designed for maximum workability, suitable for large-scale pours.
The following table provides a relative suitability guide for different PCE characteristics based on project requirements.
| Project Type | Key Requirement | PCE Characteristic | Priority Factor |
|---|---|---|---|
| High-Rise Building | High Strength | High Water Reduction | Compaction Density |
| Road Pavements | Workability | High Fluidity | Slump Retention |
| Precast Elements | Fast Turnaround | Rapid Setting | Early Strength |
| Dam Construction | Heat Control | Low Heat Hydration | Mass Compatibility |
| Marine Structures | Corrosion Resistance | Ultra-Low Chloride | Permeability |
| General Housing | Cost Efficiency | Balanced Performance | Adaptability |
Traditional superplasticizers like naphthalene-based agents rely on electrostatic repulsion to disperse cement particles. PCE, however, employs steric hindrance through long polymer side chains. This creates a more robust physical barrier between particles, allowing for significantly higher water reduction rates (often exceeding 25%) and better slump retention without increasing the water-to-cement ratio.
The recommended dosage generally falls between 0.10% and 0.40% of the cementitious material. However, the exact amount must be determined through trial mixes. Factors such as the chemical composition of the cement, the type of aggregates, and the desired slump all influence the dosage. It is critical to balance water reduction with the risk of segregation or excessive retardation.
Yes, PCE is highly compatible with supplementary cementitious materials (SCMs). In fact, it is often preferred in mixes with high fly ash or ore powder content because it can maintain fluidity despite the increased surface area of the fines. This adaptability helps in producing high-performance, sustainable concrete with lower carbon footprints.
Overdosing PCE can lead to several issues: excessive retardation of the setting time, causing delays in formwork removal; segregation of the aggregate from the paste; and in some cases, excessive air entrainment. It is essential to follow the technical specifications and perform slump tests to ensure the dosage is optimized for the specific materials used.
By allowing a drastic reduction in mixing water, PCE increases the compaction of the hardened slurry. This results in a denser microstructure with fewer interconnected pores, which improves the concrete's resistance to chloride penetration and sulfate attack. Additionally, it helps reduce shrinkage and creep, thereby decreasing the likelihood of structural cracks over time.
PCE powder should be stored in a cool, dry, and well-ventilated area. It must be kept away from direct sunlight and protected from moisture, as it is hygroscopic. Typically packaged in paper-plastic composite bags, it has a shelf life of about 12 months. If the product exceeds its shelf life, it must be re-tested for effective content and water reduction capability before use.
The integration of Polycarboxylate Ether into modern construction has fundamentally changed the possibilities of concrete design. By shifting the focus from simple water reduction to a precise control of steric hindrance and material adaptability, engineers can now create structures that are stronger, more durable, and more sustainable.
For those seeking a reliable partner in chemical additives, choosing a manufacturer with a proven track record in R&D and customized production is essential. Whether it is optimizing the water-to-cement ratio for a high-rise or ensuring the durability of a marine pier, the right PCE formulation is the key to long-term structural success.